LiFePO4 Battery Manufacturer in China: How to Vet a Factory
LiFePO4 Battery Manufacturer in China: How to Vet a Factory
China builds the lion’s share of the world’s lithium iron phosphate cells, and for a buyer chasing a reliable lithium battery manufacturer, that density is both an opportunity and a trap. The opportunity is mature supply, fast prototyping and competitive cost. The trap is that “factory” is a loose word—many trading companies rent a showroom and resell someone else’s pack. This guide gives B2B buyers a concrete vetting sequence so you sign with a real assembler, not a middleman with a good deck.
Why LFP sourcing converges on China
LFP chemistry is capacity-hungry to make and benefits from economies of scale that few regions outside China have built. Cell fabs, BMS chip houses, connector suppliers and pack lines sit within a day’s drive of each other in the Pearl River Delta and Yangtze corridors, which is why a sample can move from drawing to bench in days. That same density, however, means the barrier to calling yourself a “manufacturer” is low. Treat the country as a sourcing advantage, not a quality guarantee—your diligence is what converts the advantage into a dependable supply. A buyer who skips vetting because “it’s China” usually learns the hard way that the cheap quote was a reseller margin stacked on a reseller margin.
The two factory archetypes: assembler vs trader
Understand which animal you are talking to before you negotiate. A true assembler owns cell incoming-inspection, welding, BMS firmware and test benches; a trader sources packs from a contract line and adds a logo. Both can deliver, but only the assembler can re-qualify quickly when a cell model changes or a certification needs updating. Ask for the building address and a live video walk of the production floor—not a marketing video. A trader will deflect; an assembler will happily show you the line because it is their competitive edge. Probe with a technical question about BMS balancing current or weld penetration depth; a trader’s sales engineer will hedge where an assembler’s will answer in numbers.
Factory audit checklist
| Audit area | What a credible assembler shows |
|---|---|
| Cell incoming inspection | Sorting reports by capacity and internal resistance, batch trace codes |
| Welding & assembly | Automated spot/ultrasonic welding, torque-controlled assembly |
| BMS engineering | In-house firmware team, CAN/RS485 configurability |
| Test & aging | Charge/discharge aging benches, thermal chamber |
| Traceability | MES linking each pack serial to cell batches |
| Certifications | Current test reports: UN38.3, IEC 62619/62133, UL where needed |
A battery application solutions partner should treat this table as routine, not a burden. If a supplier cannot walk you through three of these areas with evidence, you are likely talking to a reseller. Score each area 1–5 and set a hard floor: any supplier below 4 on cell inspection, BMS or certifications is disqualified regardless of price.
Certifications that actually matter for LFP
For stationary and industrial LFP, IEC 62619 is the workhorse safety standard; for portable and medical, IEC 62133 governs cells and packs. UN38.3 is non-negotiable for transport, and North America leans on UL 1642 (cells) and UL 1973 (systems). The EU wants CE plus the relevant EN standards and RoHS substance limits. Request the actual test report PDF, not a certificate of conformity screenshot—reports name the exact model, and a cert that references a different pack is worthless. For buyers watching roadmaps, ask how the supplier handles semi-solid-state battery and sodium-ion battery programs, because chemistry transitions are where certification lag quietly kills a launch.
Cell grade verification
Grade-A cells arrive with tight capacity and internal-resistance bands and traceable batch codes. Grade-B or recycled cells are cheaper but age unevenly and are the usual source of early warranty claims. Insist on seeing the incoming sorting report: reputable lines sort cells into ±2% capacity and ±3 mΩ bands before welding. A factory that “doesn’t bother with sorting because the cells are already good” is telling you it ships unmatched cells—and unmatched cells cap the whole pack at the weakest member’s capacity. For a home energy storage system, that mismatch shows up as premature capacity loss you will be blamed for.
BMS and engineering depth
The BMS is where cheap packs fail expensively. Confirm the supplier runs its own BMS firmware team rather than buying a generic module it cannot modify. You want over/under-voltage, over-current, short-circuit, over-temperature protection and active balancing, plus a communication bus your host device can read—CAN J1939 for vehicles, RS485/Modbus for stationary, SMBus for portable. A BMS that cannot report state-of-health over the bus is a black box you will regret during a field failure. Ask to see the BMS configuration tool; if there is none, the firmware is someone else’s and you are locked to that vendor’s roadmap.
Production traceability and MES
Ask how a pack traces back to its cells. A real assembler uses an MES (manufacturing execution system) that binds each serial number to the specific cell batches, BMS firmware version and test results. This matters when one pack fails in the field: traceability turns a mystery into a one-line root cause and a targeted recall instead of a blanket return. It also deters the supplier from quietly swapping cell grades between orders—your audit trail catches it. Request a sample trace record during the pilot; if it is a spreadsheet someone typed by hand, the “MES” is theater.
Red flags during negotiation
- Refusal to share a live factory walk or test reports “for confidentiality.”
- A price far below market for the stated grade—Grade-B rarely announces itself.
- No cell-sorting data and no MES story.
- Pressure to skip the pilot run and go straight to a full PO.
- Vague answers on which lab issued the certification and for which model.
Pricing traps and how to avoid them
The cheapest quote that quietly drops to Grade-B cells is the most expensive pack you will ever buy. Negotiate on volume and design reuse, not on cell grade. Watch the “standard 100 Ah” claim—measure it; some suppliers rate at a low C-rate where capacity looks bigger. Bundle the charger, enclosure and certification scope into one quote so you compare total landed cost, not a seductive per-Wh cell price that balloons once the BMS, IP-rated case and paperwork are added. Build a simple cost model: cells (50–60%), BMS (10–15%), enclosure and labor (15–25%), certs and logistics (5–10%); a quote that breaks these rules in your favor usually hides a shortcut.
IP protection and NDA for private label
If you are private-labeling, a mutual NDA plus a contractual non-resale clause for your territory is the floor, not the ceiling. Confirm the factory will not sell your exact pack to a competitor in your region, and that reference designs are not already shipping to a direct rival. Define warranty in cycles at a stated depth-of-discharge, not just months—”24 months” can mask a 300-cycle pack behind a calendar that outlasts the cells. A short IP clause costs nothing and prevents painful disputes a year later when a copycat appears in your market.
Logistics, lead time and MOQ
Typical custom-pack MOQs start around 100–200 units; reference designs can go lower. A realistic timeline is engineering review (2–3 days), prototype (5–7 days), validation and tooling (1–2 weeks), then mass production in 15–25 days depending on cell inventory. Build your schedule around the worst-case component lead time, and pre-agree a pilot of 20–50 units before the full PO. Remember UN38.3 documentation travels with the shipment, so fold compliance into the unit cost from day one rather than discovering the DG fee at the port.
Sample testing protocol you control
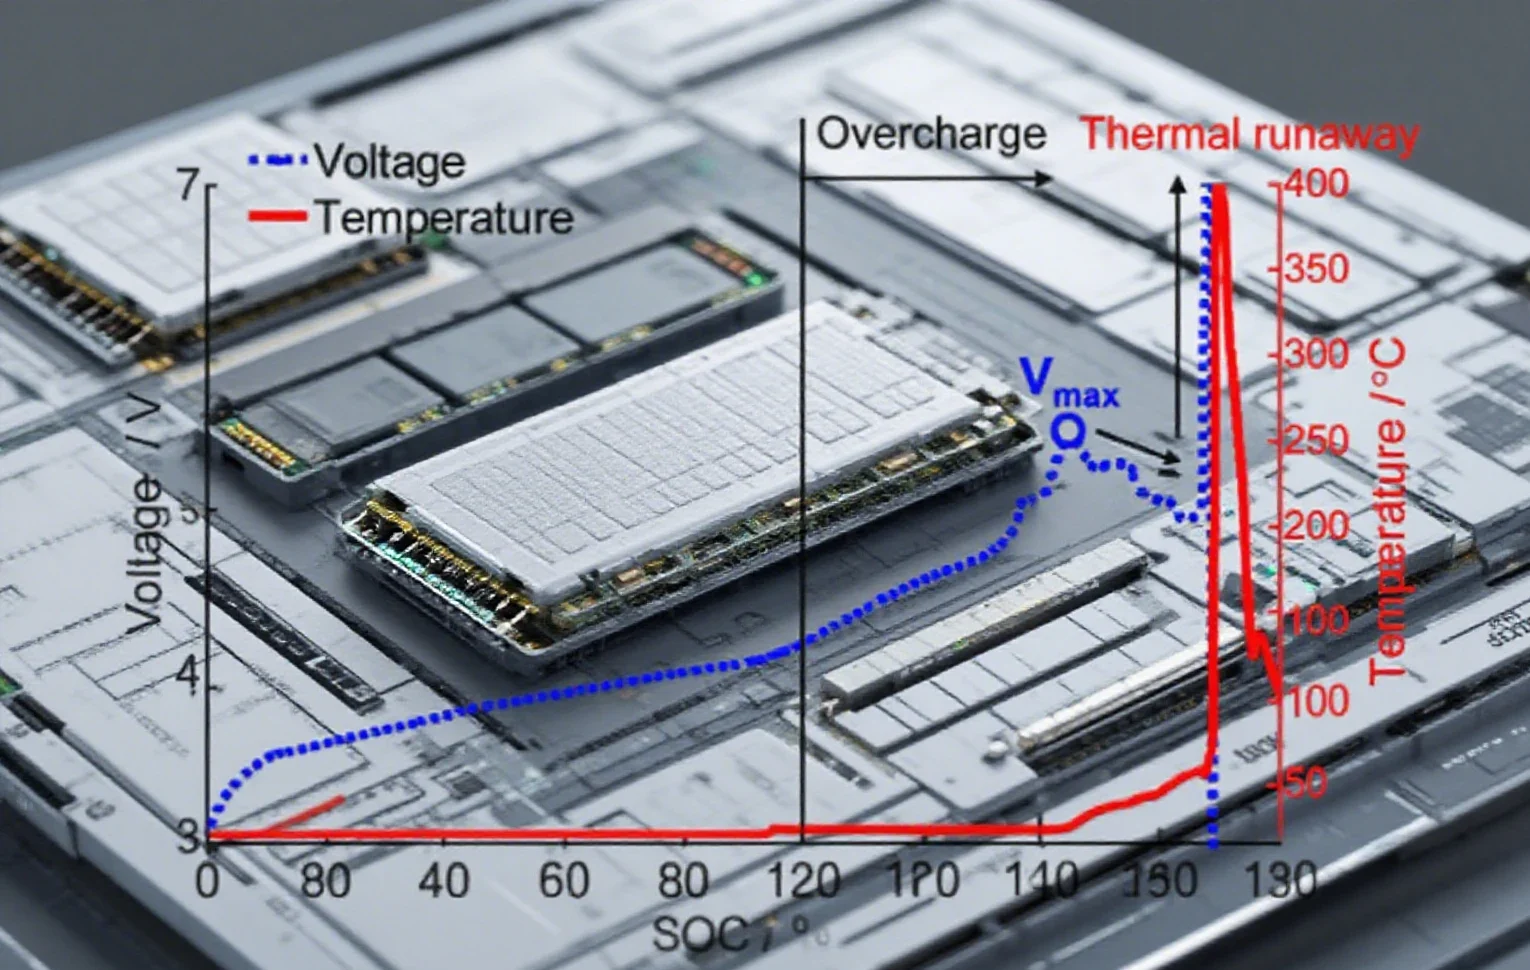
Do not trust the supplier’s capacity claim. On receipt, discharge a sample at your real load profile to cutoff and log voltage and temperature. A simple rig catches most Grade-B and mislabeled shipments before they reach your line. Keep the records; they are your evidence if a supplier silently changes the bin between orders. Three samples per batch, tested at the rated C-rate, is a low-cost insurance policy that pays for itself the first time it intercepts a bad lot.
Building a dual-source strategy
Even a well-vetted supplier is a single point of failure. Once your design is locked, qualify a second assembler on the same spec so a fire, flood or policy shift at the first does not stop your line. The second source need not win every PO; it just needs to be ready. Share the design but hold the tooling key, so neither supplier can hold you hostage. This discipline is what separates resilient supply chains from fragile ones when the market tightens.
A practical vetting sequence
- Shortlist 3–4 suppliers by public certs and visible engineering.
- Run a video audit using the checklist above; eliminate resellers.
- Request samples from the top two; independently test capacity and thermal behaviour.
- Validate the pilot run against your real duty cycle, not a bench spec.
- Sign with the supplier whose documentation and support survived scrutiny.
Frequently asked questions
Can a Chinese factory hold my IP safely? Yes, with a mutual NDA and a non-resale clause; verify they are not already shipping your design to a regional competitor.
How do I confirm the cells are really Grade A? Demand the incoming sorting report and independently test a sample; capacity and internal resistance tell the story.
Is a lower price always a red flag? Not always, but a price far below peers for the same grade usually means a silent downgrade in cells or BMS.
Do I need to visit in person? A live video walk covers most checks; an in-person audit pays off only at volume or for safety-critical programs.
Written by Karl at China Battery Technology. Send us your target spec and we will vet the build with you—request a quote and our engineers will return a design review within 24 hours.
Related Reading
- custom lithium battery manufacturer
- Lithium Ion Battery Cells Wholesale: Grades, MOQ and Pricing
- OEM Lithium Battery Pack: From Prototype to Mass Production