Battery Application Solutions for Plywood and Veneer Mill
Battery Application Solutions for Plywood and Veneer Mill
A panel mill is a study in two very different electrical problems living under one roof. The peeling and drying line wants steady, continuous heat and a long conveyor that must never stop unexpectedly, while the hot press wants enormous bursts of power for short, precisely timed cycles. Serving both from one supply is expensive; serving both from one well-designed battery application solutions package is usually cheaper per panel produced, because the buffer absorbs the press pulses instead of forcing the grid or a generator to.
The Two Loads That Define the Mill
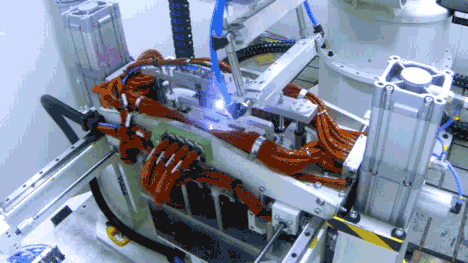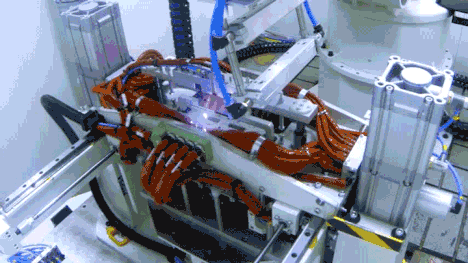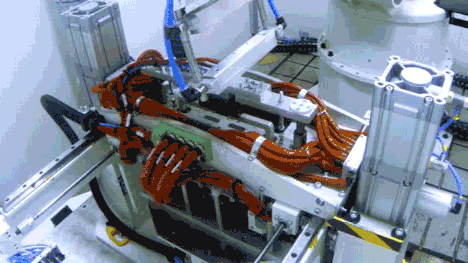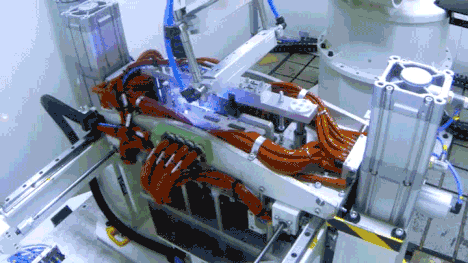
On the wet end, the peeler lathe, the clipper and the conveyor train run a fairly flat load for hours. Interruptions here are costly because veneer in process dries out, curls or jams the tray system. On the dry end, the hot press cycles: pumps and heaters ramp hard for a minute or two, hold, then release. The press is what sets the site’s demand charge and what makes an otherwise adequate supply look undersized.
Buffering the Hot Press Cycle
Storage in parallel with the press sees the ramp and supplies the difference for those sixty to ninety seconds, then recharges during the hold. The effect on the incoming supply is a near-flat line where there used to be a sawtooth. In practice this lets a mill run an additional press shift or a faster cycle on an unchanged connection, which is the outcome management actually cares about.
| Attribute | Battery buffer | Oversized generator | Grid upgrade |
|---|---|---|---|
| Handles press pulses | Yes | Poorly | Yes |
| Lead time to deploy | Weeks | Weeks | Months–years |
| Demand-charge impact | Strong reduction | None | None |
| Fuel and upkeep | None | High | None |
| Scalable in stages | Yes | Poorly | No |
Protecting Veneer in Process
Continuity matters more than autonomy on the wet end. A stop that lasts ninety seconds can leave a ribbon of veneer stranded in the dryer at temperature, which becomes waste or a quality downgrade. Put the lathe drive, the clipper, the tray system and the dryer exhaust fans on a backed-up bus configured for ride-through, so momentary dips never propagate into a process stop and a clean-down.
Heat, Resin and the Battery Room
Mills are hot and carry airborne resin acid and fine wood dust. The battery needs its own environment: a sealed, filtered enclosure in a separate room held below 30 °C, with positive pressure so dust is not drawn in through the glands. Do not site the cabinet where it shares air with the press pit, and do not share the room with resin storage.
Staging the Investment
One advantage of storage is that it scales in blocks. A mill can start with a buffer sized for the largest press, measure the demand-charge reduction over a quarter, then add capacity for the drying line or a second press with real numbers in hand. Generators and supply upgrades do not offer that option — you buy the full capacity up front or you do the project twice.
Measuring Success in Cost Per Panel
The right metric is not kilowatt-hours stored, it is energy cost per cubic metre of panel shipped and the number of process interruptions per month. Track both before and after. Mills that do this consistently find the interruption count falls faster than the energy bill, and that is usually where the quality and throughput gains are hiding.
What to Ask a Supplier
Ask for the press-cycle load profile the design is based on, the surge rating across the full ambient range of a mill building, the filtration and ingress specification for wood dust, and a staged expansion path that does not strand the first block of capacity. Then ask for two reference sites with presses of comparable cycle time.
People Also Ask
Can a battery really cover a hot press cycle? Yes. Press ramps are short and repeatable, which is exactly the duty a power-dense battery handles best.
Do we still need to upgrade our supply? Often not. Removing the press pulses from the incoming profile is frequently enough to stay within an existing connection.
How much capacity is typical? A single press line usually needs a power-dense system in the 200 kWh to 500 kWh range, with the inverter sized on the ramp rather than on the energy.
What about the drying line? Put it on ride-through rather than full backup; preventing a ninety-second stop is worth far more than running the dryer for hours.
Written by Karl at China Battery Technology. Request a quote.